TwinWorks
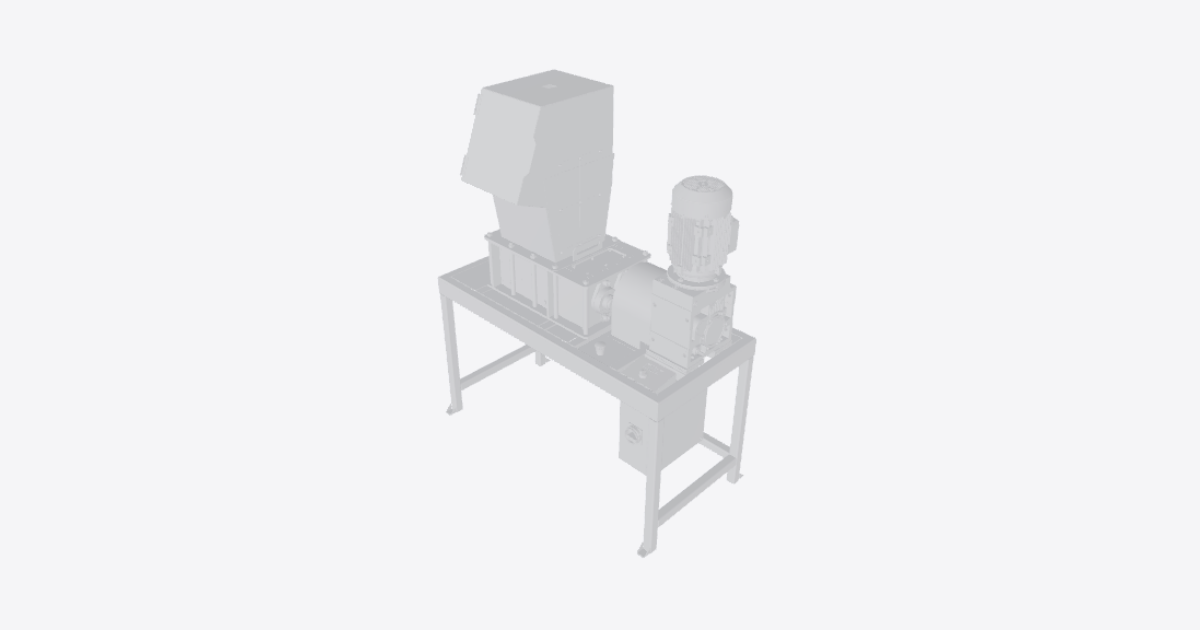
Precious Plastic shredder – 3D model preview

Precious Plastic shredder

Téa · Industrial · 3D model · Updated 6 Nov 2026

Open in 3D

  • Procedures4shared publicly
  • Views0all time
  • Rating–No ratings yet
  • Likes0from the Community

0 comments

Procedures

1. Shafts and blades

Assembly · 6 steps · No ratings yet

6 steps
  1. Prepare the two blade shafts

    Build the shafts and blades as the first assembly stage of the Precious Plastic Shredder Pro V1. Work on the loose components before installing either shaft in the shredder.

    Identify Shaft 1 for the 6-tooth blades and Shaft 2 for the 13-tooth blades. Use shafts made from 50 mm C45 hexagonal bar, turned to 45 mm at the bearing ends. Clean the hexagonal sections, bearing ends and nut threads. Remove burrs without changing the mating dimensions.

    Keep every blade and spacer clean and burr-free throughout assembly: the blade gap is only 0.25 mm.

    Credit: based on the Precious Plastic Shredder Pro V1 by Precious Plastic / One Army (preciousplastic.com), licensed CC BY-SA 4.0 (creativecommons.org/licenses/by-sa/4.0). Adapted by TwinWorks; this guide is shared under the same licence.

  2. Assemble Shaft 1: 6-tooth blades and spacers

    Support Shaft 1 so that it cannot roll. Clean and deburr the 6-tooth blades and spacers, including the hexagonal bores and all mating faces.

    Slide the components onto the hexagonal section one at a time, matching the axial order and blade orientation shown in the 3D model. Fit blade numbers 1 through 12, then repeat 1 through 12, using two of each blade. Do not put identical blade numbers next to each other.

    At the end adjacent to the first blade 1, start with a 4 mm end spacer. Between successive blades, fit a 4 mm spacer followed by a 2.5 mm spacer when progressing from blade 1 toward blade 12. Continue the same spacing between the two sets of twelve blades. Finish with the 4 mm end spacer after the second blade 12.

    Seat each component flat against the preceding component. Keep the blade indexing exactly as shown; do not force a blade over a burr or trap debris between faces. The animation shows the stack moving together for clarity; fit the physical components individually.

  3. Lock the Shaft 1 blade stack

    Fit the two DIN 1804 M50x1.5 slotted round nuts, one at each end of the blade stack on Shaft 1. Start each nut by hand without cross-threading.

    Restrain the shaft without loading the cutting edges. Tighten each nut to at least 100 Nm. Check that both nuts bear against the end spacers and that the stack is fully seated, with no loose components.

  4. Assemble Shaft 2: 13-tooth blades and spacers

    Support Shaft 2 so that it cannot roll. Clean and deburr the 13-tooth blades and spacers, including the hexagonal bores and mating faces.

    Slide the blades and spacers onto the hexagonal section one at a time, reproducing the axial positions and angular indexing shown in the 3D model. The model shows 23 blades on this shaft. Preserve their staggered orientation rather than aligning all teeth.

    Use the shown 4 mm and 2.5 mm spacers in their individual positions, including the end-spacer arrangements. Do not copy Shaft 1's end arrangement onto Shaft 2. Seat each component flat and keep all faces free of debris and burrs.

    The animation shows the stack moving together for clarity; fit the physical components individually.

  5. Lock the Shaft 2 blade stack

    Fit the two DIN 1804 M50x1.5 slotted round nuts, one at each end of the blade stack on Shaft 2. Start each nut by hand without cross-threading.

    Restrain the shaft without loading the cutting edges. Tighten each nut to at least 100 Nm. Check that both nuts bear against the end spacers and that the stack is fully seated, with no loose components.

  6. Inspect and identify the completed shafts

    Inspect the completed Shaft 1 assembly and Shaft 2 assembly. Check blade order and angular indexing against the shown stacks. Check that every blade and spacer is clean, burr-free and seated flat, and that both round nuts on each shaft are tight.

    Retain the 0.25 mm blade-gap requirement for the later installation of the shafts together. Do not assess the running gap by turning these loose shafts against one another.

    Identify the 13-tooth shaft for the recommended motor-side position and the 6-tooth shaft for the opposite side. Keep both assemblies supported and clean for the next assembly stage. Installation in the shredder is outside this procedure.
2. Cutting box

Assembly · 13 steps · No ratings yet

13 steps
  1. Position the bottom plate

    Build the cutting box as stage 2 of the Precious Plastic Shredder Pro V1, after completing the shafts and blades. Assembly reference: 1100.00 and BOM, Precious Plastic / One Army, CC BY-SA 4.0.

    Place the bottom plate on a stable, level support with its mating faces clean and the cutting chamber opening unobstructed. Orient it as shown, with the bearing-plate mounting features aligned along the shaft direction. Keep the assembly unpowered throughout this procedure.

  2. Locate the fixed-knife side plates

    Locate the two fixed-knife side plates, 1110.03 and 1110.04, against the bottom plate in the orientation shown. Align their locating features and the threaded-rod holes. Support the plates so that they cannot tip, and leave the joints loose for alignment.

  3. Fit the 51 fixed knives

    Fit the 47 fixed knives of 6 mm thickness and the four fixed knives of 4 mm thickness into the side-plate locations shown. Follow the individual positions and orientations of the 3D arrangement; do not substitute one thickness for the other.

    Seat every knife fully in its locating features, with the cutting profile facing the cutting chamber. Keep fingers clear of the sharp edges and retain the knives while the box remains open.

  4. Introduce the completed shafts and fit the bearing plates

    Support the two completed blade-shaft assemblies from the preceding procedure and introduce them into the open cutting box in the positions shown. Keep the blade stacks assembled and preserve their orientation. Do not attempt to force a completed blade stack through a bearing-size opening.

    Pass the shaft journals through the six bearing side plates, 1110.05 to 1110.10, while locating the plates around the shafts and against the box. Match the different plate profiles to their individual positions shown. Keep the top open and the plates loosely located until the shafts and all plate features align.

  5. Insert the M12 rods and tube spacers

    Insert the ten M12 threaded rods through the aligned box holes: six rods of type 1110.14 and four rods of type 1110.15, in their respective positions shown.

    Fit the ten tube spacers, 1110.13, around the rods between the upper and lower plate locations. Keep every tube square to its seating faces. Do not draw misaligned plates together by tightening the rods.

  6. Fit the top plate

    Lower the top plate over the threaded rods and onto the side plates, bearing plates and tube spacers. Align all locating features before seating the plate fully.

    Check that the fixed knives remain seated and the shaft assemblies are supported without being trapped against a plate. Keep fingers out of the closing joints.

  7. Tie the box together with the M12 nuts and washers

    Fit the M12 nuts and M12 washers to the threaded-rod clamping points. Start the nuts by hand and bring them into contact progressively, alternating between opposite positions so that the box seats evenly.

    Keep the box square and the plate joints fully seated. Stop if tightening distorts a plate or causes binding; correct the seating and alignment before continuing. Leave final alignment to be checked with the bearings installed.

  8. Fit the bearing and housing spacers

    Fit the bearing spacers over the exposed shaft journals in their individual positions shown: the two 6 mm spacer types, 1100.06 and 1100.07, and the 1 mm spacers, 1100.08. Preserve the stack order at each shaft end.

    Locate the twelve bearing housing spacers, 1100.05, at the flange mounting holes as shown. Keep the shaft spacers distinct from the small housing spacers. Ensure all seating faces are clean before bringing the bearings into place.

  9. Mount the six UCFL209 flange bearings

    Slide the six UCFL209 flange bearings over the shaft journals to their mounting positions shown. Align each flange with its mounting holes and spacer stack while keeping the shaft assemblies supported.

    Seat the bearings without hammering through the rolling elements or using mounting bolts to pull a misaligned bearing into place. Keep the mounting holes accessible for the twelve M16 bolts.

  10. Secure and align the bearing mounts

    Install the eight DIN 912 M16 × 35 bolts and the four DIN 912 M16 × 25 bolts, with the twelve washers, in the individual locations shown. Use one washer under each bolt head and retain the housing spacers in their modeled positions. Start every bolt by hand.

    Bring the mounting bolts down evenly while maintaining shaft alignment. Complete the box-rod clamping progressively, then secure the bearing mounting bolts without distorting the flanges. Check for binding as the joints are secured; do not use power to overcome resistance.

  11. Select and position the sieve

    Select the sieve, drawing 1140.00, for the required flake size: 7, 10 or 14 mm holes. Use only one hole-size option at a time. The illustrated assembly uses the 10 mm mesh pair.

    Support the complete sieve below the cutting chamber and bring it into the mounting position shown. Align its side mounting holes with the box plates. Keep the perforated surfaces clear of the rotating blades and retain support until the mounting fasteners are fitted.

  12. Fasten the sieve beneath the box

    Insert the four M10 × 40 sieve mounting bolts through the aligned side holes and fit the four M10 nuts in the positions shown. Support the sieve while starting and securing the fasteners.

    Tighten the joints evenly so that the sieve sits securely without twisting. Remove the temporary support only after all four mounting points are secure.

  13. Inspect the completed cutting box

    Inspect the top and bottom plates: confirm that all side and bearing plates are seated, the box is square, and the threaded-rod joints are secure. Check that all 47 fixed knives of 6 mm and four fixed knives of 4 mm remain correctly located.

    Confirm that all six flange bearings and their spacers are seated, the eight M16 × 35 and four M16 × 25 bolts have their twelve washers, and the selected sieve is secured at all four mounting points.

    With the drive disconnected, check shaft movement slowly from the exposed shaft ends, keeping hands out of the cutting chamber. Stop at any binding or unintended blade, knife or sieve contact. Remove loose hardware and debris. This completes the cutting-box assembly only; do not run the unguarded cutting box.

3. Gears, motor and coupling

Assembly · 10 steps · No ratings yet

Warning: Never run the motor until the hopper, sieve and coupling cover are fitted.

10 steps
  1. Prepare for the gears, motor and coupling assembly

    Carry out this third assembly stage after the cutting-box work, with the gear seats accessible for axial fitting. Keep the motor electrically isolated throughout assembly. Do not reach between the blades or meshing gears.

    Prepare the module 6 gears, keys, motor mounting plates, geared motor, HRC 230 coupling, taper locks, bearing-to-coupling spacers and coupling cover. Keep their mating surfaces clean and remove burrs before fitting.

    Never run the motor until the hopper, sieve and coupling cover are fitted.

  2. Fit the two gear keys

    Seat the two A14×9×70 parallel keys in the gear-end keyways. Fit one to the drive shaft for the 18-tooth gear and the other to the second blade shaft for the 20-tooth gear. Ensure both keys sit flat without rocking and leave the gear keyways free to slide over them.

  3. Fit and mesh the 18- and 20-tooth gears

    Slide the 18-tooth gear onto the keyed drive-shaft end and the 20-tooth gear onto the other keyed shaft end. Align each hub keyway with its key and bring both gears to their seated positions without hammering the teeth.

    The gears are module 6 with 114 mm between shaft centres. Align their tooth faces and mesh them in the orientation shown. With the motor isolated, turn the shafts slowly by hand from a safe accessible shaft end. Confirm that both shafts turn together in opposite directions without binding or blade contact. Keep fingers out of the gear mesh.

  4. Position and bolt the motor mounting plates

    Arrange the four motor mounting plates as two stacks of two plates beneath the gearbox mounting feet, matching the positions shown. Align the plate holes with the mounting points and bolt the plates in place. Keep the plate faces seated flat and preserve adjustment for motor-to-shaft alignment.

  5. Fit the bearing-to-coupling spacers

    Slide the two 1 mm spacers onto the drive-shaft end first, followed by the 10 mm spacer. Seat the stack against the outside bearing, with the 10 mm spacer towards the coupling. Fit these rings before the coupling key and hub, keeping all spacer faces flat against one another.

  6. Fit the drive-side coupling key, hub and taper lock

    Seat the third A14×9×70 key in the coupling-end keyway of the drive shaft. Fit the drive-side HRC 230 coupling half with the 3020-45 taper lock over the shaft and key, outboard of the spacer stack.

    Align the taper-lock fitting holes with the hub holes and engage its clamping screws. Keep the hub adjustable until the motor-side half is aligned. Do not use the coupling to pull misaligned shafts together.

  7. Mount the geared motor and join the coupling

    With the geared motor securely supported and electrically isolated, fit the motor-side HRC 230 coupling half and its 3020-40 taper lock to the gearbox output shaft. Preserve the output-shaft key engagement and keep the hub adjustable.

    Mount the 2.2 to 4 kW geared motor on the plate stacks. Support its weight independently while bringing its output shaft into line with the drive shaft. Bring the coupling halves together with the HRC flexible element correctly seated, without forcing them together or transferring motor weight through the coupling.

    Start the M10×40 mounting bolts and nuts, leaving enough freedom for final alignment.

  8. Align the drive and secure the motor and taper locks

    Adjust the geared motor on its mounting plates until the two coupling halves are concentric, their faces are parallel and the flexible element is not compressed by incorrect hub spacing. Maintain clearance between rotating hubs and stationary parts.

    Tighten the motor mounting bolts and nuts evenly. Tighten the taper-lock clamping screws progressively and alternately. Recheck alignment after tightening.

    With electrical isolation maintained, turn the drive slowly by hand from a safe accessible shaft end. Stop if the gears, blades or coupling bind. Do not use motor power for this check.

  9. Fit and fasten the coupling cover

    Position the coupling cover over the assembled coupling. Seat its mounting edges and fasten it with M10×40 bolts and nuts. Ensure the cover is secure and does not touch either rotating coupling half.

    Keep the motor isolated. Do not operate the shredder with the cover removed or loose.

  10. Complete the unpowered assembly check

    Check that both gears are seated on their keys and mesh across their tooth faces. Check that the geared motor is firmly mounted, both taper locks are secure, all three bearing-to-coupling spacers are seated and the coupling cover is fastened with clearance from rotating parts.

    Remove loose assembly items from the drive area and leave the motor electrically isolated. This assembly stage does not include electrical connection or a powered test.

    Never run the motor until the hopper, sieve and coupling cover are fitted.

4. Hopper, frame, electronics and safe use

Assembly · 11 steps · No ratings yet

Tools

  • push tool

Protective equipment

  • dust mask
  • safety glasses
  • ear protection

Warning: Only a licensed professional may work inside the electrical box.

Warning: Electrical hazard: only a licensed professional may work inside the electrical box.

Warning: The machine needs a 16 A breaker.

Warning: Never run the machine without the hopper and sieve fitted.

Warning: Do not wear gloves when operating the shredder.

Warning: Never push plastic in with your hands. Use the push tool.

11 steps
  1. Prepare for final assembly

    Complete the frame, hopper, electronics and safe-use stage of the Precious Plastic Shredder Pro V1. Keep the machine disconnected from its electrical supply throughout mechanical assembly.

    Use either the basic hopper (1200.00) or the closed safety hopper (1300.00), not both. This procedure illustrates the closed safety hopper.

    Attribution: Precious Plastic / One Army, official drawings, BOM and shredder instruction manual, CC BY-SA 4.0.

  2. Fabricate the frame, 1410.00

    Build the frame (1410.00) from 40 × 40 × 3 mm and 40 × 80 × 3 mm steel tube, using the illustrated member arrangement.

    1. Cut and deburr the tube members. Prepare the joints and mounting holes.
    2. Fixture the members on a flat surface. Check that the legs and crossmembers are square and the mounting faces align.
    3. Tack the joints, recheck alignment and complete the welds without pulling the frame out of square.
    4. Remove sharp edges and weld spatter. Check that the frame stands without rocking and that the mounting holes remain accessible.
  3. Position and anchor the frame

    Position the frame on a sound, level floor with at least 2 m clear all round the machine. Keep access to the controls and emergency stop unobstructed.

    Use the foot mounting holes to mark the anchor positions. Drill and install M8 floor-fixing hardware suitable for the floor, then bolt the machine down. Check that all feet are supported and the frame cannot rock or shift.

  4. Secure the cutting box to the frame

    Keep the completed cutting box supported while aligning its mounting rods with the frame. Seat the box fully on the mounting faces without trapping any cables.

    Fit the six lower M12 nuts shown beneath the mounting points. Tighten them progressively and evenly, keeping the box seated and aligned. Release the support only after the box is securely fixed.

  5. Seat the selected hopper on the cutting box

    Fit the closed safety hopper (1300.00), or use the basic hopper (1200.00) instead. Install only one hopper.

    With the hopper mounting nuts still off, support the hopper above the cutting box. Align its base holes with the mounting rods and lower it onto the top mounting face. Keep fingers clear of the joint and check that the base sits flat without forcing it.

  6. Fasten the hopper with M12 nuts

    Keep the hopper supported and fully seated. Fit the four M12 hopper mounting nuts shown at the corners of its base.

    Start the nuts by hand, then tighten progressively in a diagonal pattern so that the base remains flat. Check that the hopper cannot lift or rock. On the closed safety hopper, check that the door, window and handles are secure and that the door closes correctly.

  7. Mount the electronics box on the frame

    Keep the supply disconnected. Support the electronics box (1420.00) at the side of the frame in the illustrated position. Align it with the frame's mounting brackets and secure it before releasing the support.

    Keep the controls accessible and route cables clear of moving parts, sharp edges and the floor. Leave the enclosure closed unless a licensed electrical professional is carrying out the electrical work.

  8. Complete the electrical installation, licensed professional only

    Only a licensed electrical professional may work inside the electronics box. Isolate the supply and prove it dead before opening the enclosure.

    Install and connect the Arduino Nano reverse circuit, two contactors, motor protection breaker, emergency stop and main switch. Provide a supply protected by a 16 A breaker. Complete protective earthing, cable restraint and the required electrical safety tests before energising.

    Close and secure the enclosure after the work. Do not energise an incomplete or untested installation.

  9. Complete the pre-start safety check

    With the supply isolated, check that the hopper is secure and the sieve is fitted. Never run the shredder without both the hopper and sieve installed.

    Check that all guards and frame covers are secured, the electronics box is closed, the floor fixings are tight and the 2 m clear area is unobstructed. Remove loose tools and offcuts from the machine.

    Wear a dust mask, safety glasses and ear protection. Do not wear gloves. Keep loose clothing, hair and jewellery away from the feed opening and moving parts.

  10. Test the controls before feeding plastic

    With the hopper and sieve fitted, all guards secured and everyone clear, energise the machine for an empty functional test.

    Check normal start and stop, the reverse function and the emergency stop. After operating the emergency stop, check that releasing it alone does not restart the machine. Stop the test if any control behaves unexpectedly, the frame moves or abnormal vibration or noise occurs. Isolate the supply before correcting a fault.

  11. Feed safely and shut down

    Keep the hopper and sieve fitted throughout operation. Keep the 2 m clear area free and the emergency stop accessible.

    Feed plastic gradually. Never push plastic in with your hands: use the push tool and keep your hands outside the hopper. Wear a dust mask, safety glasses and ear protection, and do not wear gloves.

    Stop feeding before shutdown, stop the machine and isolate the supply. Wait until all motion has stopped before cleaning or clearing a blockage. Never reach into the cutting area while the machine can start, and never open the electrical box unless you are a licensed electrical professional.

Related products

  • Precious Plastic extrusion machine

    Téa

    Industrial · 3D model · 4 procedures

    No ratings yet

    0 likes · 0 comments · 0 views

  • Helicopter Rotor

    Mina

    Industrial · 3D model · 1 procedure

    No ratings yet

    0 likes · 0 comments · 1 view

  • V8 Engine

    Mina

    Industrial · 3D model · 1 procedure

    No ratings yet

    0 likes · 0 comments · 0 views

  • Boxer Engine

    Téa

    Industrial · 3D model · 1 procedure

    No ratings yet

    0 likes · 0 comments · 2 views